Exhaust air filtration
and
heat recovery
for megacasting
We are the experts for environmental technology in large-scale casting: smoke extraction, exhaust air filtration, and heat recovery for die casting machines beyond 5,000 tons — in use worldwide in gigacasting and megacasting foundries.
Think big. Cast green.
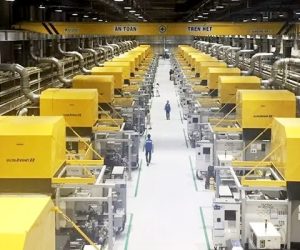
Megacasting changes the scale. Larger clamping forces, larger molds — and a corresponding amount of smoke and oil aerosol with every cycle.
For 30 years, we have been capturing and filtering emissions from die casting machines. Now we are scaling this experience for solutions on molds in the meter scale and clamping forces beyond 5,000 tons.
Capture. Filter. Recover heat. Our systems intervene at three points: at the cell with an extraction hood or air curtain system, in the flexibly placeable filter system — and at the decentralized melting furnace, where most of the energy is located.
Extraction at the source is the most efficient way:
A concentrated exhaust air flow can be cleaned with a fraction of the effort that large volumes of air in hall ventilation would cost. At the same time, oil mist is kept away from machines, robotics, and the hall construction — and out of your employees’ breathing air.
We plan emission protection and heat recovery as one system.
Investing in the megacasting cell is the right moment for this.
Secure your green competitive advantage.
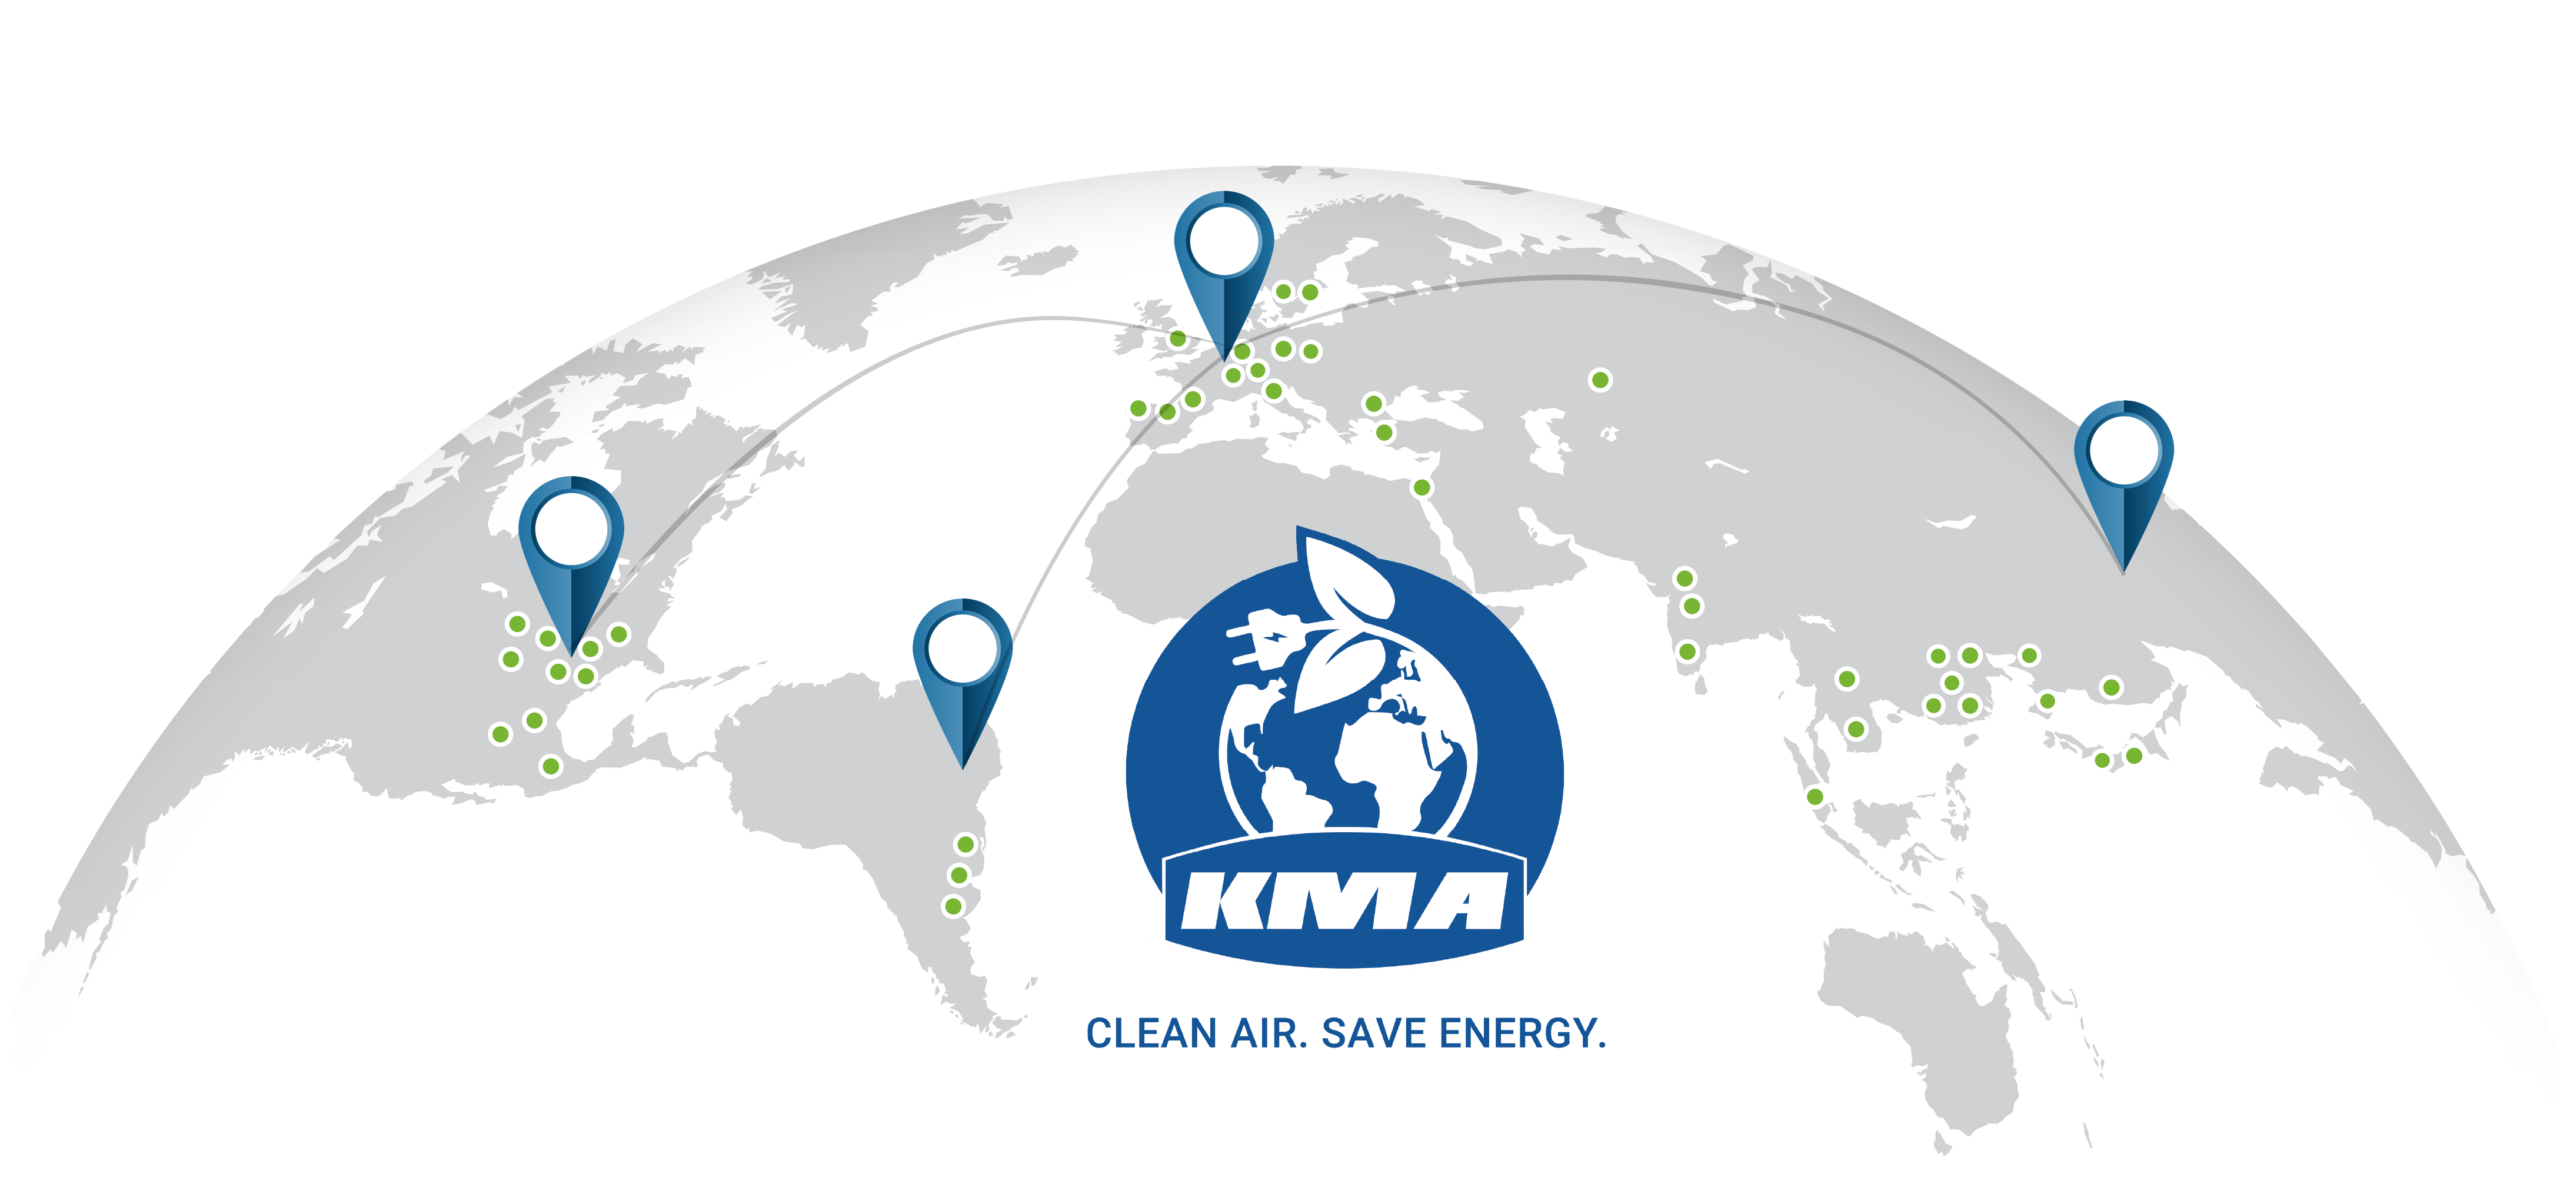
13 established megacasting locations worldwide.
No one brings more Gigacasting experience to the table. The industry’s best-practice projects set the standard — and are being transferred to new megacasting locations with KMA. Let this valuable experience flow into your project.
Meet emission requirements below EU BAT levels
Increase energy efficiency of the entire site
Improve air quality & maintain investment value
We put our trust in KMA
Megacasting scales your production. We scale your energy efficiency.
Foundry planning and environmental technology from a single source: Megacasting becomes successful when hall layout, material flow, media supply, and environmental technology work together from the start.
KMA combines its expertise in smoke extraction, exhaust air filtration, and heat recovery with the know-how of experienced foundry planners like Klaus Hansen, founder of ODIN Casting Solutions. This results in integrated, energy-efficient solutions for high-performance megacasting sites.
Experience from best-practice projects, which are considered the benchmark in the industry, thus flows directly into your design. Where the extraction hood is located, how the filters are placed, and how the waste heat can be used at the site is decided in the early planning phase.
(Photo from left to right: Dr Holger Wagner, KMA, Klaus Hansen, Odin Ltd.)
Think big. Cast green.
Emissions, exhaust air and energy. Engineered together.
Anyone planning megacasting is planning energy flows. The waste heat from a melting furnace is of a magnitude that can supply the entire production site — hall heating, process heat, neighboring trades. Whether this potential is tapped is not decided when buying a filter, but in the planning phase. That is why we work together with factory planners and foundry architects from the first layout sketch.
One technical solution, three tasks:
Extraction hoods or air curtain systems capture emissions directly at the cell.
The ULTRAVENT® filter system cleans the exhaust air — flexibly placeable.
At the melting furnace, the hot exhaust air becomes an energy source for your site — usable for hall heating, process heat, or adjacent trades in a magnitude of 2 to 4 GWh per year.
You are currently viewing a placeholder content from YouTube. To access the actual content, click the button below. Please note that doing so will share data with third-party providers.
More Informationclean air.
save energy.
>3,000
Systems installed worldwide
80 %
Energy savings possible compared to conventional exhaust air technology
360°
Emissions, exhaust air and energy. Engineered together.
1,500 +
Customers worldwide trust our technology
Solutions for energy-efficient megacasting
Proven KMA solutions designed for clamping forces over 5,000 t
Large machines require extensive extraction. From a clamping force of 5,000 tonnes upwards, the width and length of the hoods increase — and with them the volume of exhaust air required for reliable smoke extraction.
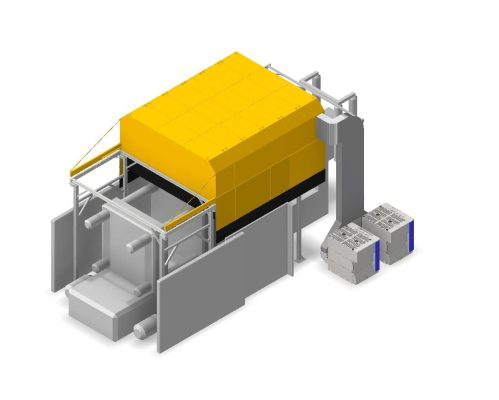
A fume extraction hood or air curtain system captures emissions at the Gigacasting cell, whilst the energy-efficient ULTRAVENT® filter system purifies the exhaust air.
In megacasting, we use the KMA ULTRAVENT® III in pairs: 2 x 15,000 or 2 x 20,000 m³/h. While one device filters, the other cleans itself automatically. Extraction continues — without production interruption, without filter replacement.
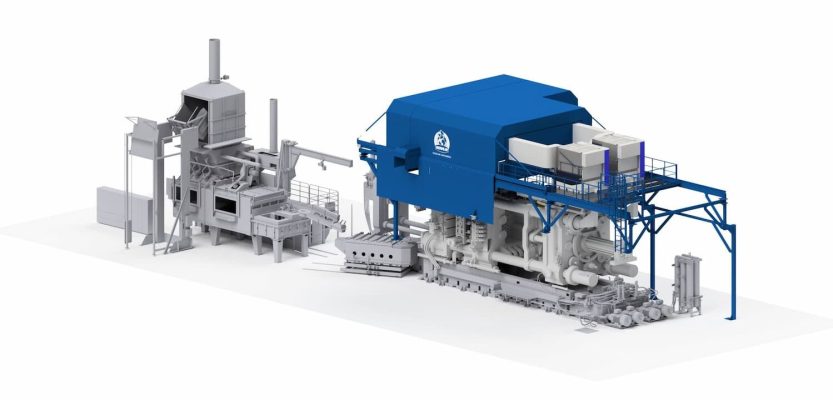
Megacasting with extraction hood and ULTRAVENT III exhaust air filter
Effective smoke extraction in megacasting
The hood must capture the smoke and keep the machine accessible. The casting cells are structured very differently — each setup needs its own answer to where the hood ends and accessibility begins. Two-part hoods enclose the cell during operation and move apart for tool changes. Which division fits is decided by crane guidance, casting unit, and space on site.
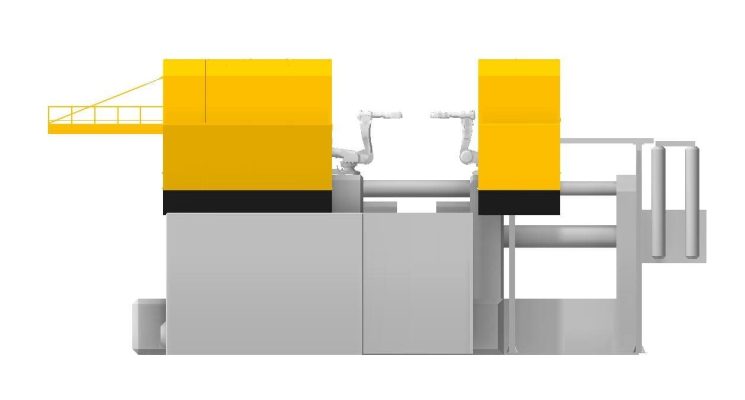
Two-part hood – partially stationary
Only one hood part moves, the other remains fixed — usually on the side of the casting unit. This keeps hood length, travel path, and static loads low and allows the connection of service platforms on a fixed plate.
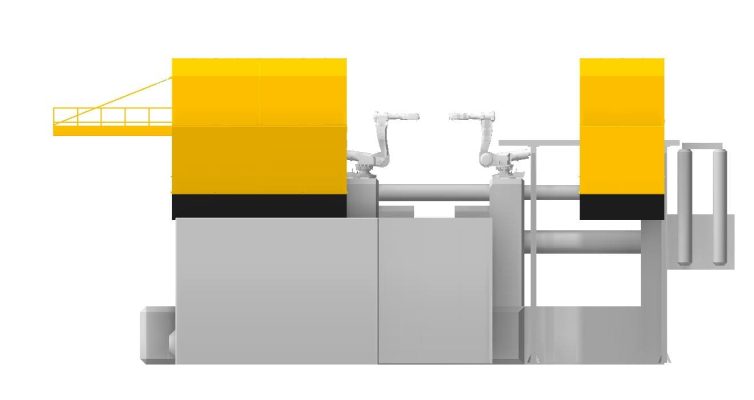
Two-part hood – movable on both sides
Maximum accessibility: Both hood parts move apart on rails. Crane and tool changes reach the machine from both sides — with full extraction efficiency during operation.
Flexible placement of filter systems
Every hall is different. The ULTRAVENT® III adapts — for the best possible arrangements for filter and extraction hood.
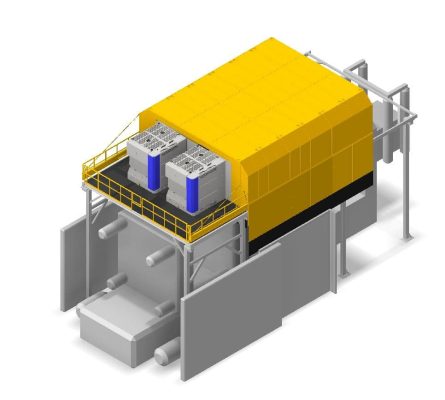
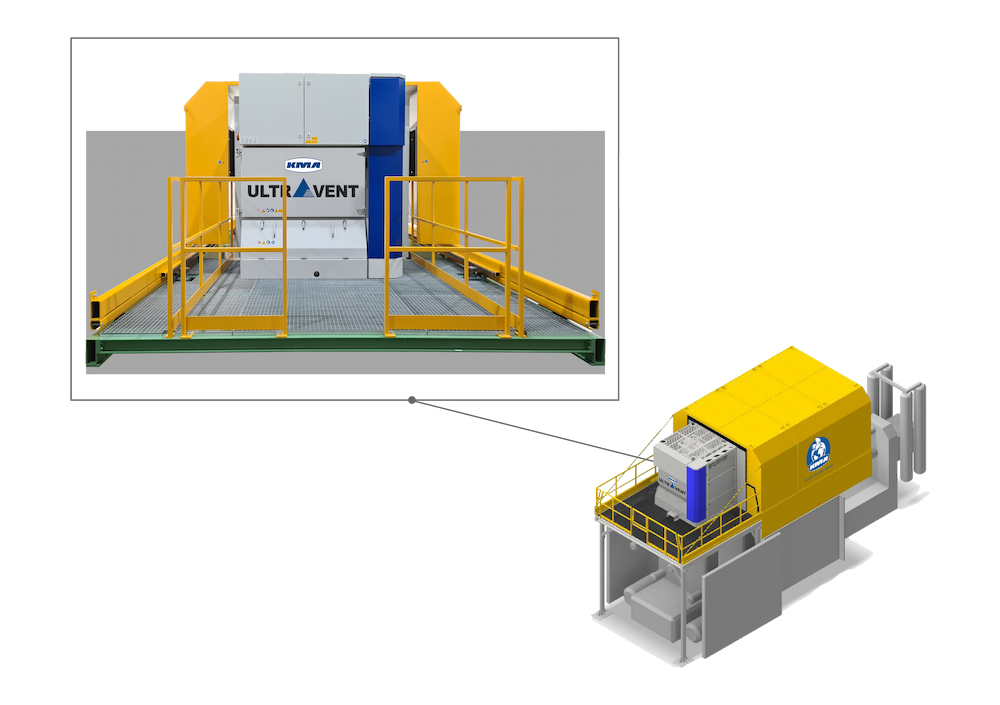
Rear connection of the ULTRAVENT® III exhaust air filter
The most energy-saving arrangement: The exhaust air filter sits directly on a service platform above the clamping unit — shortest paths, minimal pressure drop, no additional space required in the hall. The movable extraction hood moves back over the filter.
Side connection of the ULTRAVENT® III exhaust air filter
The solution for limited overall height: The exhaust air filter stands on the operator level or service platform next to the machine. Access to the clamping unit remains free — for improved accessibility of the die casting machine with the hall crane.
ULTRAVENT® III:
The efficiency exhaust air pro for die casting
The exhaust air professional also works in megacasting. The ULTRAVENT® III was developed for energy-efficient exhaust air filtration on die casting machines — at the gigacasting cell, it filters according to the same principle, only on a larger scale.
For over 30 years, our environmental technology engineers at KMA have been developing bespoke systems for smoke extraction, exhaust air purification and heat recovery in foundries.
Frequently asked questions about exhaust air filtration in megacasting
What makes exhaust air filtration in megacasting more demanding than on classic die casting machines?
The dimension changes the task: larger machines, larger extraction space, more exhaust air. Added to this is the variety of casting cells and peripherals — one, two, or four spray robots, area gantries, and more — while at the same time having high requirements for the accessibility of the die casting machine for hall cranes and lifting equipment. Complex, automated casting cells in limited space: Here, experience decides which solution really fits.
When do you recommend an extraction hood, and when an air curtain system?
The hood is our recommendation as soon as the installation space allows it; we recommend the air curtain system if overall height, crane paths, or accessibility requirements rule out a hood. In both cases, extraction takes place directly at the source. The hood concept has been proven for many years: emissions are physically captured, the hood acts as a buffer tank that is extracted during the casting cycle and whose exhaust air is filtered — most effective extraction rate, best energy efficiency. The air curtain guides a horizontally adjustable air flow over the cell to the opposite extraction unit: working area and crane path remain free, less material and thus lower transport costs — but a higher extraction capacity. For each cell, we choose the principle where extraction rate and accessibility match.
How much megacasting experience does KMA have?
We know megacasting projects across the industry — KMA technology is in use today at 13 locations worldwide, with very different starting situations: casting cells with one to four robots, with and without spray gantries, machines from various DCM manufacturers, greenfield planning as well as expansion in an existing foundry. We have realized not only extraction and filtration at the die casting machine, but also exhaust air filtration and heat recovery at melting furnaces as well as the hall ventilation of entire sites — with the interfaces to the casting cell, melting furnace, ventilation technology, and fire protection. This is relevant because spraying processes, number of robots, cell layout, and furnace technology significantly change the exhaust air situation: every site needs its own design. The basis is 30 years of emission extraction on die casting machines and over 2,000 systems for the die casting industry, scaled to clamping forces beyond 5,000 tons. In research and development, we cooperate with the GTK Kassel, the Center for Lightweight Casting and Construction — we are happy to establish contact with reference sites.
Your direct contact
Talk to Kerem Kartal
Would you like to know how cell-level collection, exhaust air filtration and heat recovery can be effectively combined in large-scale casting operations?
Then let’s work together to determine which system design is best suited to your site, both technically and in terms of energy efficiency. The starting point is always the actual layout of your production hall.
Our die casting solutions in the trade press
Publications & technical articles
We are the expert
Further applications
More information
Downloads & links
Laws & guidelines
TA-Luft: Air pollution control – emission limit
VDI 2262-3: Workplace air quality – pure-air recirculation
TRGS 900: Workplace limit values